
Please Choose Your Language
Views: 157 Author: Site Editor Publish Time: 2026-09-02 Origin: Site
Transitioning from manual grinding to automated finishing requires more than just plugging in equipment. Modern fabrication facilities demand high throughput and precise edge quality. For production managers and facility buyers, understanding how to properly use and integrate a deburring machine is critical. Operational mastery ensures consistent part quality while reducing scrap rates. You must control variables like feed speed and abrasive wear to achieve repeatable results.
This guide breaks down the operational realities, standard procedures, and implementation factors required to deploy automation successfully. We will explore setup steps, calibration routines, safety compliance, and troubleshooting techniques. You will learn exactly how to configure equipment for a high-volume manufacturing environment.
Method dictates operation: Operational procedures vary heavily depending on whether you are using a wide-belt, rotary brush, or tumble deburring system.
Calibration is continuous: Consistent edge quality requires strict management of feed speeds, abrasive wear, and part-thickness calibration.
Safety requires infrastructure: Proper usage mandates integrated wet or dry dust extraction systems to mitigate combustible metal dust risks.
Evaluate before you scale: Understanding daily operational requirements helps facilities accurately shortlist machines based on tooling changeover times and automation capabilities.
Implementing a successful edge finishing strategy begins by identifying your core application. You must clarify whether your primary goal is heavy slag removal, uniform edge rounding, oxide layer removal, or surface finishing. Each objective demands a different mechanical approach. Selecting the right metal deburring machine establishes the foundation for your entire production workflow.
Machine operations generally fall into three distinct categories. Wide-belt systems excel at removing vertical burrs and applying straight-line graining. They require precise thickness calibration to avoid removing too much base material. Rotary brush systems provide uniform, multi-directional edge rounding. They handle complex geometries exceptionally well. Tumble or vibratory systems process bulk batches of small, fragile, or highly complex parts.
The "best" machine always depends on your upstream processes. Fiber lasers produce different burr profiles than plasma cutters. Plasma-cut edges often feature hard dross. Fiber-cut edges might just have sharp micro-burrs. Your dimensional tolerances will ultimately dictate which system yields acceptable finished parts.
Primary Application | Recommended Machine Type | Ideal Upstream Process |
|---|---|---|
Heavy Slag & Dross Removal | Wide-Belt System (Coarse Grit) | Plasma or Oxy-Fuel Cutting |
Multi-Directional Edge Rounding | Rotary Brush System | Fiber Laser or Waterjet |
Bulk Processing of Small Parts | Tumble/Vibratory System | Punch Press or Small Laser |
Straight-Line Surface Graining | Wide-Belt System (Fine Grit) | Shearing or Precision Laser |
Standardizing your operating procedures minimizes operator error and protects equipment longevity. We recommend following a strict sequence every time you power up the machine. This step-by-step approach guarantees optimal surface finishes across every batch.
Step 1: Pre-Operation Inspection & Setup
Always verify the condition of abrasive belts, brushes, or tumbling media before starting a shift. Damaged abrasives ruin parts instantly. Next, ensure your dust extraction system is active. Verify it functions at the proper CFM (Cubic Feet per Minute) to evacuate hazardous particulate.
Step 2: Material Measurement and Machine Calibration
Measure the exact thickness of your sheet metal or part batch using digital calipers. Adjust the machine's contact rollers and brush heads to match this specific material thickness. Accurate calibration prevents over-grinding, part rejection, and excessive wear on conveyor belts.
Step 3: Setting Feed Rates and Spindle Speeds
You must balance the conveyor speed against the aggressiveness of your selected abrasive. Slower feed rates yield heavier radiusing and deeper surface penetration. Faster feeds prioritize throughput but may leave slight micro-burrs. Adjust spindle speeds to match the material hardness.
Step 4: Test Runs and Quality Verification
Never run a full production batch immediately. Process a sacrificial part or a small sample batch first. Inspect these samples carefully. Look for uniform edge rounding, surface finish consistency, and signs of thermal distortion. Adjust settings as necessary.
Step 5: Continuous Production and Monitoring
Once production begins, monitor the amperage loads on the grinding heads. A sudden spike in amperage often indicates premature abrasive wear or motor strain. Address load warnings immediately to prevent mechanical failures.
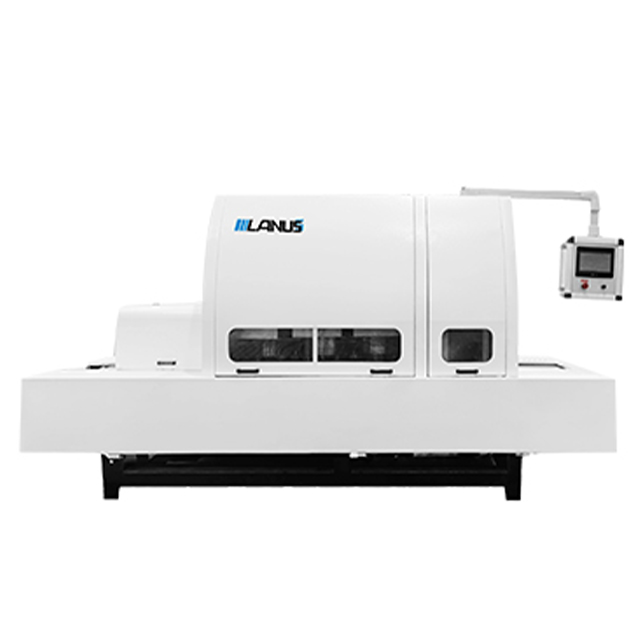
Consumables account for a significant portion of your ongoing operational workflow. Effective abrasive lifecycle management keeps production moving predictably. You need a reliable system to track the wear of belts and rotary blocks. Operating a machine while using dull abrasives increases heat transfer into the workpiece. This excess heat risks warping thin sheet metal permanently.
Tooling changeovers also impact daily productivity heavily. You should evaluate the operational downtime required to switch between different grits or brush materials. For example, switching from carbon steel processing to stainless steel requires a complete abrasive swap to avoid cross-contamination. Operators need quick-change tooling systems to minimize this necessary downtime.
If you utilize vibratory systems, media selection becomes your primary focus. You must match ceramic, plastic, or organic media to the metal's specific hardness. Choosing the wrong media leads to parts lodging together or surface impingement. Plastic media works well for softer metals like aluminum. Ceramic media aggressively cuts harder steels.
Media Type | Best Suited For | Common Mistake to Avoid |
|---|---|---|
Ceramic | Hard metals (Carbon steel, Titanium) | Using on soft aluminum (causes heavy pitting) |
Plastic | Soft metals (Aluminum, Zinc die-casts) | Expecting heavy burr removal (it only polishes/radiuses) |
Organic (Walnut/Corn) | Final polishing and light drying | Using for actual burr removal (it lacks cutting power) |
Industrial metal finishing generates distinct hazards. Combustible dust management ranks as the highest priority. Processing aluminum and titanium creates highly volatile dust particles. Proper usage mandates strict compliance with National Fire Protection Association (NFPA) and OSHA standards. You must utilize compliant wet-type dust collectors or specialized dry filtration systems equipped with explosion isolation valves.
Cross-contamination presents another severe operational risk. You must enforce strict separation between carbon steel and stainless steel or aluminum processing. Mixing carbon steel sparks into a dust collector containing aluminum dust creates an immediate fire hazard. Additionally, carbon particles embedded in stainless steel surfaces will cause rapid galvanic corrosion later.
Machine safeguarding protects operators from catastrophic physical injuries. Belt machines utilize anti-kickback fingers to prevent parts from shooting backward out of the feed area. You must verify these fingers move freely before every shift. Emergency stops must remain easily accessible. Finally, implement rigorous lockout/tagout (LOTO) procedures during every abrasive replacement or internal maintenance task.
Even highly calibrated automated systems occasionally produce suboptimal results. Operators must diagnose and resolve surface finish issues quickly to maintain throughput. Understanding the root causes of common defects empowers your team to make immediate mechanical adjustments.
Uneven edge rounding typically stems from uneven conveyor belt wear. If operators repeatedly feed parts down the exact center of the conveyor, the center track degrades faster than the edges. Improper part placement also causes this issue. You must calibrate brush heads regularly to ensure they apply uniform pressure across the entire working width.
Thermal distortion ruins thin-gauge sheet metal. This warping results from excessively slow feed speeds combined with aggressive grits. When degraded, dull abrasives generate excess friction instead of shearing metal away. To fix this, increase your conveyor speed or replace loaded belts immediately. Utilize a wet system if your application constantly involves extremely thin materials.
A secondary burr occurs when an abrasive belt folds the metal over rather than cleanly shearing it off. This usually means the abrasive grit is too fine or the belt speed is incorrect. Resolving this often requires adjusting the belt speed. Alternatively, transition to a multi-head machine configuration. A primary belt removes the vertical burr, and a subsequent rotary brush cleanly sweeps away any remaining secondary burrs.
Purchasing the correct equipment dictates long-term success. Begin by assessing footprint and facility requirements. Note the power requirements, specifically voltage and maximum amperage draw. Evaluate the physical floor space available. Remember to account for the necessary dust collection footprint, which often matches the size of the machine itself.
Next, evaluate throughput versus automation needs. You must decide whether a manual-feed standalone unit or a fully integrated line yields the best return. Automated lines utilize return conveyors and robotic loading arms. They require higher upfront planning but drastically reduce labor dependencies.
Deciding between dry and wet processing fundamentally changes your maintenance routine. Dry machines offer easier daily maintenance but require strict, code-compliant dust management. Wet machines feature built-in cooling and inherent dust mitigation. However, they require diligent coolant filtration and regular sludge disposal management.
The most reliable way to validate machine efficacy is through sample part processing. Submit your own cut parts directly to the OEM. Request test runs using various grits and speeds. Seeing your exact materials processed provides irrefutable proof of capability before you commit to a purchase.
Operating automated finishing equipment demands consistent calibration, strict abrasive lifecycle management, and rigorous safety compliance.
Successful implementation starts by perfectly matching the machine configuration to your specific metalworking processes and upstream cutting methods.
Never mix combustible metals without dedicated, code-compliant dust extraction systems in place.
Audit your current manual grinding hours and scrap rates to establish a baseline for improvement.
Contact an application engineer today to schedule a time-study or submit your parts for sample processing.
A: Mechanically, yes. Most machines easily adjust to process both materials. However, mixing metals creates severe safety hazards. Aluminum dust mixed with carbon steel sparks poses an extreme explosion risk. You must either use a wet-type dust collector, thoroughly clean the machine between runs, or dedicate separate machines entirely.
A: Replacement frequency depends on material hardness, initial burr size, and daily throughput hours. Heavy dross removal on steel might require belt changes weekly. Light edge rounding on aluminum allows brushes to last for hundreds of hours. Operators should track amperage loads; a spike indicates abrasives need replacing.
A: It depends on the chosen configuration. Rotary brushes strictly target edges and rarely alter core material thickness. Wide-belt systems, especially those using coarse grits for heavy slag removal or surface graining, will remove a slight layer of the base material. Precision calibration prevents excessive thinning.
A: The learning curve is relatively short. Modern equipment features CNC-style controls and programmable recipes. Once an engineer or experienced manager saves the ideal feed speeds and brush depths for a specific part, everyday operators simply select that recipe and feed the parts, drastically lowering required skill levels.


